 LKprototype
the delivered batch. Where a drawing or purchase order requires an EN 10204 Type 3.1 inspection certificate, that requirement is a specification item, not a courtesy.
A usable certificate ties three things together: the specified alloy and condition, the heat or batch number, and the parts you received. If the alloy matches but the heat number cannot be connected to your lot, the certificate proves that the correct material exists somewhere, not that it is in your parts.
Traceability becomes more complex when materials or processes pass through multiple hands. Heat treatment, plating, and passivation are commonly subcontracted, and each hand-off is a place where lot identity can be lost. Ask how the supplier maintains lot identity across outsourced processes, and ask for the process certificates for those operations where they are relevant.
INSPECTION REPORTS AND QUALITY RECORDS
The question to settle at quoting stage is what documentation arrives with the shipment, because retrofitting a documentation requirement onto a completed order rarely works. Typical items are a certificate of conformance, a dimensional inspection report, material certificates where specified, and process certificates for subcontracted operations.
Two negotiation points are worth raising early. First, whether documentation is included or priced separately — a supplier that treats inspection reports as an upsell item and a supplier that treats them as standard output are not equivalent partners for production work. Second, what records are retained and for how long, since your own traceability obligations may extend beyond the delivery date.
For prototype orders, the documentation scope can reasonably be lighter. A dimensional report on critical characteristics and a material certificate where the material matters are usually enough to validate a design. For production, the full chain — material, process, inspection, and conformance — is what protects you during a customer audit or an internal quality investigation.
HOW TO EVALUATE ENGINEERING AND DFM SUPPORT
DRAWING AND CAD REVIEW BEFORE QUOTING
The strongest single indicator of engineering capability is whether the drawing is reviewed before the price is written. A supplier that quotes from the model alone may miss what only the drawing states: critical characteristics, datum requirements, finish specifications, and inspection expectations.
Test this directly. Send an RFQ with a deliberate ambiguity or a demanding tolerance and see what comes back. If the response identifies the ambiguity or questions the tolerance, the review happened. If the response is a price with no questions attached, the supplier either assumed an interpretation or did not read carefully — and either way, the same assumption will apply during production.
Some suppliers will quote fast and correctly on straightforward parts without questions, and that is a legitimate outcome. The relevant test is whether questions appear when the part warrants them. A complex part that generates no questions is a warning sign, not a bargain.
TOLERANCE AND DATUM REVIEW
Tolerance review is where an engineering-capable supplier earns its margin. Two things should come back. First, a statement of which characteristics the supplier considers critical and why — usually the functional ones: mating features, sealing surfaces, locating bores, and assembly interfaces. Second, a comment on any tolerance that appears to drive cost without driving function.
GD&T deserves particular attention. Position and profile tolerances are interpreted through a datum reference frame, and an ambiguous or conflicting datum scheme creates a real manufacturing risk. A supplier that raises the question before production is protecting your schedule. A supplier that resolves the ambiguity silently has made a design decision on your behalf.
For critical features, the drawing should also make inspection visible: which characteristics will be measured, with what method, and in what state — constrained or free. If the design has a feature whose measurement method is unclear, that should be resolved during DFM review rather than during first article disposition.
MATERIAL AND FINISH RECOMMENDATIONS
A supplier that only machines what you specify is providing a service. A supplier that comments on material and finish selection is providing engineering.
Useful recommendations are conditional rather than directive: for this geometry and load case, a different aluminium alloy would machine more stably; for this cosmetic surface, anodizing would conceal tool marks that as-machined finish would expose; for this corrosion environment, the specified stainless grade may pit where a molybdenum-bearing grade would not. Each of these statements should come with the reason attached, because that is what makes it checkable.
Material availability is a legitimate part of the conversation. A specification that requires a grade or condition with long mill lead times has a schedule consequence, and raising that at quoting stage is more useful than discovering it three weeks later.

IDENTIFYING MANUFACTURING RISKS EARLY
Early risk identification is the difference between a DFM conversation and a post-mortem. The risks that matter in CNC work are predictable: thin walls that deflect under cutting force, deep pockets that require long tools, tight tolerances on features that cannot be measured reliably, datum transfers across multiple setups, and materials that work-harden or move after machining.
A supplier with real experience will name the specific risk in your part rather than offering general observations about machining being complex. The most valuable version of this conversation ends with a decision: adjust the design, accept a cost premium for a special fixture, change the measurement approach, or run a trial cut before committing to the production quantity.
ENGINEERING COMMUNICATION DURING REVISION
Revision handling is where well-quoted projects go wrong. Ask to see how the supplier controls drawing revisions: how a revision change is received, confirmed in writing, and propagated to programming, fixturing, and inspection.
The specific failure to guard against is a shop producing to an older revision because the change arrived through a channel that did not reach programming. Written confirmation of the revision in force, on the order acknowledgement, is a low-cost control that prevents an expensive outcome. It also gives you a record showing which revision was manufactured if a question arises later.
FACTORY VS. BROKER: WHAT SHOULD BUYERS VERIFY?
A supplier that sells capacity it does not own can still deliver an excellent part. The question that matters is not whether your supplier manufactures the part itself, but whether the manufacturing and quality control arrangement is disclosed and visible enough to evaluate. CNC supplier factory verification should therefore be approached as a transparency test rather than a fraud hunt.
HOW TO CONFIRM THE ACTUAL MANUFACTURING SITE
Start with identity consistency. The company name, address, and contact details on the quote, the invoice, the quality certificate, and the shipping documentation should agree. Divergence is not automatically dishonest — companies legitimately operate through trading entities — but it needs an explanation, and the explanation should name the legal entity that will manufacture the parts and the site where that happens.
Next, ask directly where the parts will be made and whether any operations are subcontracted. A supplier confident in its arrangement will answer specifically. A supplier that deflects the question has given you the answer in a different form.
If the arrangement involves a manufacturing partner, ask what quality control responsibility the seller carries: who approves the first article, who authorises shipment, who handles nonconformance, and whose name appears on the certificate of conformance. Those answers define whether you have one accountable supplier or an unmanaged chain.
EQUIPMENT, ENGINEERING, AND INSPECTION EVIDENCE
The fastest way to understand a supplier's real structure is to ask what happens when a drawing question arises. A manufacturer answers with an engineer's name and a technical response. An intermediary usually routes the question externally and returns with a slower, less specific answer. This is not a moral distinction; it is a structural one, and it tells you where technical decision-making sits.
Evidence that a manufacturing site is real and active includes a live video walkthrough showing machines running, footage or photographs of your part in process, the metrology area with identifiable equipment, and the material receiving area. Photographs of a shop floor taken from a marketing page prove nothing; a live walkthrough of a specific machine running a specific job proves quite a lot.
For inspection evidence, ask who performs the dimensional inspection and where the report is generated. If the answer is a third-party laboratory, that is acceptable and sometimes better than an in-house bench check — but it should be stated, priced, and scheduled rather than discovered at shipment.
SUBCONTRACTING TRANSPARENCY
Subcontracting is normal in this industry. Finishing processes, heat treatment, EDM, and specialised operations are frequently outsourced by manufacturers of every size. The risk is not that subcontracting happens; it is that it happens invisibly, so that a schedule or quality problem appears without an explanation.
Ask which operations are subcontracted, which suppliers are used for them, and how those suppliers are approved and monitored. Ask how lot identity is maintained across the hand-off and what documentation comes back. Then confirm that the subcontracted operations are inside the quoted lead time and price.
Disclosed subcontracting with a clear control description is a manageable arrangement. Undisclosed subcontracting discovered later is a governance problem, because you cannot qualify what you cannot see.
Pro Tip: A live factory walkthrough can complement documentation by allowing buyers to verify equipment, inspection areas, material handling, and the actual production environment.Let's begin the tour of the LKprototype factory.
WHY BROKERS ARE NOT AUTOMATICALLY A BAD CHOICE
An intermediary can add real value: consolidating multiple processes under one purchase order, handling export documentation and logistics, providing engineering review in your timezone, and taking responsibility for supplier quality across operations you would otherwise have to manage individually.
The conditions that make this work are specific. The intermediary should disclose that it does not manufacture in-house, identify the manufacturing site or sites, state who controls quality and who approves the first article, and be willing to put that responsibility in writing. Its engineering response should be technical rather than transactional.
The arrangement becomes problematic when the intermediary presents itself as a manufacturer, when quality responsibility is ambiguous between the parties, or when the manufacturing site changes between orders without notice. In those cases the buyer has lost visibility without gaining anything in return.
PROTOTYPE VS. PRODUCTION SUPPLIER REQUIREMENTS
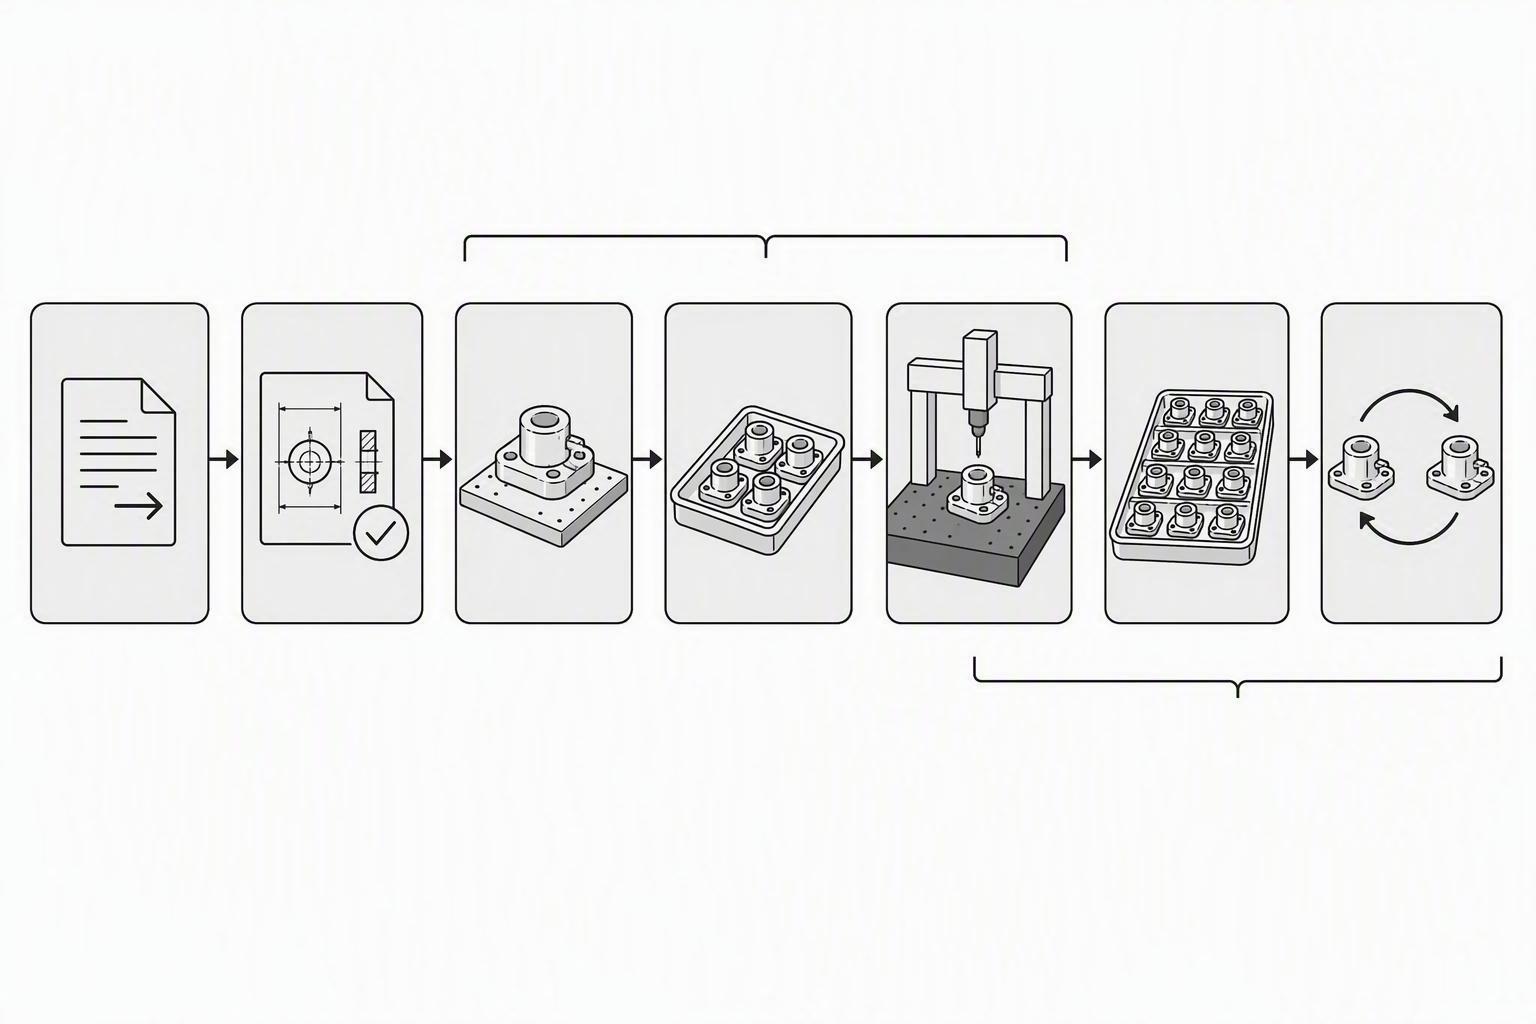
An approved prototype proves that a design can be made once. It does not prove that the supplier can make it repeatedly, at volume, with documented control. Programs derailed by this assumption are common enough that the distinction deserves its own evaluation criteria.
WHAT PROTOTYPE PROJECTS NEED MOST
Prototype work rewards responsiveness and engineering engagement more than process documentation. The priorities are technical feedback on the design, willingness to iterate, short feedback loops on questions, and flexibility when a revision arrives mid-order.
Inspection at prototype stage should be proportionate: dimensional verification of the critical characteristics, a note of any deviation found, and enough material identification to know that the part is the material you intended. Full production documentation on a prototype is usually unnecessary cost.
Speed matters, but the useful kind of speed is iteration speed — how fast a revised design becomes a revised part — not the headline number on a marketing page. A supplier that turns a prototype in four days but takes a week to answer a question about a tolerance has not actually been fast.
LKprototype's own CNC prototype machining workflow follows this stage logic: engineering review of the uploaded CAD, DFM commentary, machining, dimensional verification, and finishing, sized for functional prototype parts rather than for serial production documentation.
WHAT PRODUCTION PROJECTS NEED MOST
Production shifts the weighting decisively toward repeatability, process control, and documentation. The questions change from "can you make this part?" to "can you make this part the same way, on the same parameters, for the two hundredth time, and prove it?"
The criteria that gain weight are fixture strategy and programme control, in-process inspection with defined frequency, documented tooling and parameter control, material traceability to lot, a defined change-control process, and a documented approach to nonconformance. Capacity and delivery reliability also become structural rather than incidental, because a slipped delivery on a production order disrupts a build schedule rather than a review meeting.
Cost structure changes too: setup and programming cost amortise across the quantity, so per-part price falls — but the units that matter are the total cost of conforming parts, not the theoretical per-part price on a quote that excludes inspection.
CAN THE SUPPLIER SCALE AFTER A SUCCESSFUL PROTOTYPE?
The honest answer is that a successful prototype tells you the supplier can machine your geometry. It does not tell you whether the supplier can schedule for volume, sustain process control across a production run, or maintain inspection throughput as output rises.
Test scalability with specific questions rather than general assurances. What machine time would be dedicated? What fixtures would be built, and who pays for them? How would inspection scale — sampling plan, dedicated inspection station, or outsourced metrology? What is the maximum monthly volume the current arrangement supports? What changes at that ceiling?
A supplier that can answer these in operational terms is plausibly scalable. A supplier that answers with enthusiasm is not yet answering the question.
PILOT ORDERS AND FIRST-ARTICLE VALIDATION
Before committing to a large production order, a controlled pilot order is a proportionate way to buy information. Whether it is warranted depends on part criticality, volume, cost of failure, and how new the relationship is. A low-risk part with a well-qualified supplier may not need one; a critical component with a new supplier usually does.
What makes a pilot useful is a defined purpose and defined acceptance criteria, agreed before the order is placed: which characteristics will be inspected, against which drawing revision, with what measurement method, and what documentation accompanies the shipment. The pilot is then evaluated on dimensional results, documentation completeness, material traceability, packaging performance, communication quality, and how deviations were handled.
The last item is the most informative. Every supplier hits a problem eventually. A pilot that surfaces a small nonconformance and a clear corrective response has taught you more about the relationship than a pilot where nothing went wrong.
REVISION CONTROL AND PROCESS REPEATABILITY
Repeatability is a process property, not a machining skill. It comes from controlled programmes, defined fixtures, documented parameters, and inspection that detects drift before it becomes a rejected lot.
Revision control sits at the centre of this. There must be a single current revision, a documented route by which changes reach programming and inspection, and written confirmation of the revision in production. Where design changes arrive frequently during prototype development, the same discipline should apply at lower formality: each shipment should be traceable to the revision it was made from.
Process documentation matters for the same reason: if the parts are good and nobody recorded how they were made, the second order starts from an unknown baseline. A supplier that can hand you the programme revision, the fixture identity, and the inspection record for a production lot has given you a reproducible process, which is the asset you are actually buying.
HOW TO EVALUATE CNC SUPPLIER LEAD TIME
WHAT SHOULD A CNC LEAD TIME INCLUDE?
A quoted lead time should be decomposable into stages, and a supplier unable to decompose it is offering an estimate rather than a commitment. The stages that commonly sit inside a realistic window are engineering review and clarification, material procurement, CAM programming, setup and fixturing, machining, finishing, inspection, packaging, and shipping.
Two clarifications change the number materially. First, when the clock starts — on purchase order receipt, on drawing approval, or on material arrival. Second, which stages are inside the window and which are outside. If inspection, finishing, or shipping is outside, the delivery date you were given is not the date your parts arrive.
Ask also what would move the date: material availability, revision changes, first article approval, a change in quantity, or congestion in outsourced finishing. A supplier that can name the sensitivities has thought about the schedule. A supplier that promises the date will hold under any change has not.
MATERIAL AVAILABILITY AND PRODUCTION SCHEDULING
Material availability is the most common hidden driver of lead time, and it varies by alloy, temper, form, and dimension. A standard aluminium plate may be in stock locally while a specific stainless grade in a specific thickness requires a mill order. This is not a supplier failing; it is a fact about the material, and it belongs in the quote as an assumption.
Scheduling is the other driver. Ask how work is sequenced, whether the quoted lead time assumes a specific machine slot, and what happens if that slot moves. For repeat orders, ask whether the part can be scheduled as a standing item with reserved capacity, which is generally more reliable than re-queuing each time.
For international sourcing, add the variables that sit outside the manufacturing window: export documentation, customs clearance, and the freight schedule, including seasonal congestion in the shipping calendar. Holiday periods in both the manufacturing and the destination country can add days that no production plan accounts for.
OUTSOURCED FINISHING AND SECONDARY PROCESSES
When finishing or heat treatment is outsourced, the supplier's lead time depends on someone else's schedule, and an outside process is where a delivery date most often slips without warning. The practical questions are which processes are outsourced, what lead time those suppliers currently quote, whether they are approved or interchangeable, and how quality control covers the process.
Where a finishing process is critical to function — sealing surfaces, corrosion resistance, electrical conductivity, or dimensional effects from coating thickness — it also belongs in the inspection plan. Ask what is inspected after finishing, not just before.
SHIPPING, PACKAGING, AND DELIVERY ASSUMPTIONS
Packaging is part of the delivery scope and it is frequently under-specified until the first damaged shipment. Protective requirements depend on the part: machined surfaces, cosmetic faces, thin features, and fitted bores all need protection beyond a bag in a box. Ask what packaging is standard, whether it is adequate for your part's fragility and finish, and whether custom packaging or returnable containers are available and priced.
Then settle the delivery terms explicitly. Which Incoterm applies, who arranges freight and insurance, which port or airport, and who is responsible at each stage. For international shipments, clarify who handles customs documentation and duties, because an unclear arrangement produces delay and cost that cannot be recovered from the parts.
Two final checks worth putting in writing: the receiving hours and location, and the notification process once the shipment leaves. Small administrative gaps create deliveries that no one knows to expect, which is an expensive way to lose a day.
HOW TO COMPARE CNC MACHINING SUPPLIER QUOTES
COMPARE THE SAME RFQ AND TECHNICAL SCOPE
Quote comparison is valid only when every quote prices the same thing. Before looking at any number, confirm that each supplier quoted the same drawing revision, the same material grade and condition, the same finish specification, the same quantity and quantity breaks, the same inspection requirements, and the same delivery scope.
This is the step buyers skip when schedules are tight, and it is the step that produces wrong sourcing decisions. A quote built on a superseded revision, a different material condition, or a lighter inspection scope is not a lower price — it is a different offer.
A practical control is to send an RFQ package that states the scope explicitly: drawing revision, 3D model where available, material and condition, critical tolerances and geometric requirements, finish, quantities for prototype, pilot, and production, inspection and documentation expectations, packaging and labeling requirements, and any applicable industry or customer requirements. Suppliers who receive an unambiguous package either meet it or flag a deviation, and either response is useful.
CHECK MATERIAL, FINISHING, AND INSPECTION SCOPE
Three line items carry the most scope risk, because they are the easiest places to leave something out without it looking like an omission.
Material: the same nominal alloy in a different condition is a different proposition, and a mill certificate requirement changes both price and lead time. Confirm the specification down to temper or condition.
Finishing: whether the specified process is performed in-house or subcontracted, and whether the quote includes it. Anodizing, coating, and heat treatment are commonly excluded or estimated separately.
Inspection: how much measurement is included, using which method, and with which report. This is the single most variable element between quotes and the one most often compared as if it were constant.
If a supplier's quote does not state a scope element, ask rather than assume. An assumption made in the buyer's favour during evaluation rarely survives contact with production.
REVIEW ASSUMPTIONS AND EXCLUSIONS
Assumptions and exclusions are where the real content of a quote lives. A useful quote states the lead-time assumptions, the material availability assumption, what is excluded from inspection, what is excluded from packaging, which commercial terms apply, and how long the price is valid.
A defensible approach is to record the assumptions from each quote in a comparison sheet before ranking anything, so that a low number with caveats does not compete with a higher number that is complete. Where an assumption is unclear, ask for it in writing. Clearly documented assumptions make supplier comparison and downstream change management easier.
COMPARE TOTAL DELIVERED COST NOT UNIT PRICE ALONE
Total delivered cost is what the part costs you by the time it is usable in your building. It includes the per-part price plus one-time costs (setup, programming, tooling, fixtures, and qualification or first-article effort), plus inspection you either pay for or perform, plus packaging, freight, insurance, duties, and any buyer-side handling. Then it includes the expected cost of failures — rework, replacement, expedited shipping, and engineering time.
Comparing quotes on that basis requires a consistent structure. The table below gives one; the specific numbers are yours to fill in, and the units should be identical across suppliers.
Comparison item | What to normalize | Supplier A | Supplier B | Supplier C |
|---|---|---|---|---|
Scope lock | Drawing revision, material grade/condition, quantity basis, unit of measure |
|
|
|
Recurring unit price | Same quantity tier, same unit |
|
|
|
One-time costs | Setup, programming, tooling, fixtures, qualification, first article |
|
|
|
Inspection scope | Included method and report; any separately priced measurement |
|
|
|
Finishing | Included processes, in-house or outsourced, price basis |
|
|
|
Packaging | Standard or specified; cost basis |
|
|
|
Freight and duty | Incoterm, destination, duties, insurance |
|
|
|
Commercial terms | Currency, payment terms, quote validity, escalation conditions |
|
|
|
Lead time | Start trigger, stages included, shipping transit |
|
|
|
Assumptions and exclusions | Stated in writing by the supplier |
|
|
|
Risk allowance | Expected rework, replacement, and expedite exposure |
|
|
|
Total delivered cost | Computed on the normalized basis above |
|
|
|
Filling in the last row is where the evaluation usually changes. A supplier with a higher unit price but a complete inspection scope, disclosed finishing, and stated assumptions frequently wins on total delivered cost. The cost drivers that produce that outcome are the same ones that determine a part's price in the first place, and LKprototype's breakdown of CNC machining cost factors is a useful reference for identifying which drivers your RFQ should ask suppliers to address.
IDENTIFY SUSPICIOUSLY LOW OR INCOMPLETE QUOTES
A low quote is not automatically wrong. Genuine advantages exist: lower regional labour cost, better material purchasing, or a shop that happens to have the right machine idle. The question is whether the low number can be explained by structure rather than by subtraction.
A quote warrants scrutiny when it prices a different material grade, condition, finish, or inspection scope than the RFQ required; when it omits or buries tooling, setup, programming, inspection, or first article; when it excludes freight, duty, packaging, or buyer-side operations; when it depends on an unclear quantity break or minimum order quantity that makes the unit price non-comparable; when the supplier will not provide any cost breakdown or any stated assumptions; and when it sits far below others without an explanation that matches a real structural advantage.
⚠️ Warning: An incomplete quote is not a cheaper quote — it is a quote for less work. When the missing scope reappears later as inspection fees, finishing invoices, freight, or rework, the total delivered cost has usually already exceeded the supplier you rejected. Price the scope, then compare the price.
CNC SUPPLIER RISK AND DUE DILIGENCE
Risk evaluation is not an argument for avoiding suppliers. It is a method for knowing which risks a program is carrying and what will be done about them. Five categories cover most of what can go wrong in CNC sourcing.
QUALITY AND DELIVERY RISK
Quality risk is the probability that a delivered lot does not conform, multiplied by what that costs you. It concentrates in three places: critical characteristics that are difficult to measure, processes with poor capability for the required tolerance, and features that depend on inspection to detect drift.
Delivery risk is related but separate. It concentrates in material procurement, outsourced processes, capacity saturation, and shipping and customs. For production programs, the practical response is to define what a late shipment costs, agree on notification obligations when a schedule is at risk, and keep enough schedule buffer to absorb an ordinary disruption.
For both categories, the useful instrument is not a generic risk score but a specific question: which characteristic, which process, which supplier, and which shipment could fail, and what is the plan when it does? A supplier that can discuss this without defensiveness is a better partner than one that treats the question as an insult.
CAPACITY AND SINGLE-SOURCE RISK
Single-source dependency is a strategic exposure, and it is worth quantifying rather than assuming. If one supplier, one machine, one operator, or one subcontracted finishing house is the only route to your part, then that node carries the entire program.
Three practical mitigations exist. First, characterise the exposure: for this part, what would actually stop production — a specific 5-axis machine, a specific fixture, a specific material grade? Second, build a second source before you need it, which typically means qualifying a second supplier on a small order while the first source is still healthy. Third, keep enough external process ownership picture in your own files — the drawing revision, material specification, inspection requirement, and process sequence — that a transfer is possible without reconstructing the design intent from scratch.
Note that a second source does not have to be a second manufacturer. Sometimes it is a second approved finishing supplier, a stocked material reserve, or a duplicate fixture. The objective is removing the single point of failure, not duplicating the entire supply chain.
IP, CONFIDENTIALITY, AND DRAWING PROTECTION
Drawings, CAD models, and production information are among the most valuable assets a hardware program holds, and they are handed to suppliers routinely. The controls available are straightforward, and the failure mode is usually omission rather than technical sophistication.
Start with a non-disclosure agreement that covers drawings, models, and process information, signed before the RFQ if the design is sensitive rather than after the order. Confirm who inside the supplier can access the files, where they are stored, and whether they are transmitted over a controlled channel rather than personal messaging applications. Ask whether the supplier restricts recording devices on the shop floor, since drawings displayed on a machine controller or a fixture drawing are a real exposure path.
For particularly sensitive parts, ask whether the supplier will accept sub-assembly or blind-manufacturing arrangements that limit the visible design intent. Not every supplier can support this, and not every part needs it. The point is that IP protection should be a stated requirement with an agreed method, not an assumption that professional behaviour will cover it.
MATERIAL TRACEABILITY AND COMPLIANCE RISK
Traceability risk is the inability to prove what your parts are made from after the fact. It becomes acute in regulated industries, where material certification and process records may be audit items, and it is discomforting in any program where a material failure would be expensive to investigate.
The controls are the ones described earlier: certificates tied to lot or heat numbers, records for subcontracted processes, and a retained documentation chain that connects material and process records to specific parts. Confirm early which certificate type the specification requires, because a certificate type that the material supplier cannot produce for a particular grade or form will delay the order regardless of how well the machining is planned.
Compliance requirements beyond material — restricted substance rules, country-of-origin documentation, or industry-specific approval requirements — should be stated in the RFQ and confirmed in writing before the order, not raised at shipping.
HOW TO PLAN A SUPPLIER EXIT OR SECOND SOURCE
Planning an exit is not disloyalty; it is part of qualifying a supplier properly. A supplier relationship with no transfer path is a dependency, and dependencies should be understood when they are created rather than discovered when they are tested.
What makes a transfer possible is documentation you hold. That means the current drawing revision with clear datum and inspection requirements, the material specification with condition and certificate type, the inspection characteristics you actually care about, and any process constraints discovered during qualification. Keeping these in your own configuration control means a new supplier can be brought up without re-deriving the design intent.
Operationally, three habits reduce exit risk. Keep the qualification package current, so a second source can be evaluated against it at any time. Run occasional small orders with a second supplier to keep them warm, because qualifying a supplier under time pressure is a poor way to qualify one. And record why you chose the incumbent, including what evidence supported the decision, so a future transfer has a baseline to compare against.
CNC MACHINING SUPPLIER SCORECARD
A scorecard turns a set of impressions into a comparable record, and it forces the weighting decision to be made before the supplier conversation rather than after it. The scale below is a simple 1–5 rating applied to each dimension.
Score | Meaning |
|---|---|
5 | Evidence provided directly and completely; demonstrably stronger than required for this part |
4 | Evidence provided with minor gaps that were resolved on request |
3 | Capability plausible; evidence partial or available but with friction |
2 | Claims without supporting evidence; uncertainty remains after asking |
1 | Evidence absent, contradictory, or refused |
HOW TO SCORE SUPPLIER CAPABILITY
Capability scoring covers four sub-questions: machine and process fit for your geometry, material experience in your specific grade and condition, tolerance capability demonstrated on comparable features, and finishing and secondary operation coverage.
Score capability on evidence, not on stated ability. A supplier that identifies the specific machine, explains how the features will be reached, and supplies a dimensional report on a comparable part scores at the top of the scale. A supplier that describes its general capability without mapping it to your part scores in the middle regardless of how large the facility is.
Keep a record of what evidence supported the score. A score without an evidence note cannot be reviewed later, and the whole point of the scorecard is that it produces a defensible decision rather than a feeling.
HOW TO SCORE QUALITY AND ENGINEERING SUPPORT
Quality scoring covers the certificate and its scope, calibration management, inspection equipment relative to your tolerances, first article practice, and documentation scope. A high score requires all of these to be visible; certification alone should not lift the score on its own.
Engineering support scoring covers drawing review before quoting, quality and specificity of DFM feedback, tolerance and datum commentary, and communication during a revision. The most discriminating signal here is the RFQ interaction itself: does the supplier ask useful technical questions?
Scores in these two dimensions tend to correlate with the overall outcome of a program more strongly than price does, because they predict the cost of problems you cannot currently see.
HOW TO SCORE DELIVERY, COST, AND RISK
Delivery scoring should be based on the decomposability of the lead time and the clarity of its assumptions, not on how short the number is. A supplier that can explain the stages, the start trigger, and what would change the date scores higher than one that quotes three days with no conditions attached.
Cost scoring should reflect total delivered cost on a normalized basis rather than unit price, with the completeness of the quote treated as part of the evaluation. A transparent quote with a higher unit price and a complete scope can score higher than a low unit price with unstated exclusions.
Risk scoring captures outsourcing exposure, single-source dependency, IP handling, and traceability. This is the dimension where a score of 5 means the risk is understood and controlled — not that no risk exists, which would be untrue of any supplier.
Scorecard dimension | Supplier A | Supplier B | Supplier C |
|---|---|---|---|
Capability (machine fit, material, tolerance, finishing) |
|
|
|
Quality (certificate scope, calibration, inspection, FAI, documentation) |
|
|
|
Engineering support (drawing review, DFM, datum/tolerance commentary) |
|
|
|
Capacity (relevant machine time, scheduling, inspection throughput) |
|
|
|
Delivery (lead-time definition, assumptions, shipping scope) |
|
|
|
Communication (technical contact, clarity, revision handling) |
|
|
|
Price (total delivered cost on a normalized basis) |
|
|
|
Risk (outsourcing, single source, IP, traceability) |
|
|
|
Weighted total |
|
|
|
HOW TO WEIGHT SCORES FOR PROTOTYPES VS. PRODUCTION
The weights should follow the project, and the reason to set them in advance is to prevent the cheapest quote from quietly becoming the decision. Two illustrative weighting profiles show how the emphasis shifts; use them as a starting shape and adjust to your own program constraints.
Dimension | Prototype-weighted importance | Production-weighted importance |
|---|---|---|
Capability | High | High |
Quality | Moderate | High |
Engineering support | High | Moderate |
Capacity | Low | High |
Delivery | High | High |
Communication | High | Moderate |
Price | Moderate | Moderate |
Risk | Low | High |
Prototype projects reward engineering flexibility, feedback quality, and iteration speed. Production projects reward quality evidence, capacity, repeatability, delivery reliability, and risk control — the dimensions that determine whether the second, tenth, and hundredth shipment are as good as the first.
No weighting profile here is an industry standard, and presenting it as one would be misleading. The weights are a documented expression of your program's priorities, and their main value is that they force the priorities to be written down before the quotes arrive.
HOW LKPROTOTYPE SUPPORTS CNC PROTOTYPE AND PRODUCTION PROJECTS
The evaluation method above applies to any supplier, including LKprototype. The following describes what LKprototype publishes about its CNC work, so that a buyer can place it in the framework rather than in place of it.

ENGINEERING REVIEW AND DFM FEEDBACK
LKprototype's CNC workflow begins with an engineering review of the uploaded CAD, with DFM analysis provided as part of quoting. The review covers part design along with material, surface finish, structure, and drawing details before production. This is the same drawing-review-before-quoting behaviour described earlier in this guide, and it is the stage where manufacturing risks are supposed to surface.
CNC MACHINING FOR PRECISION PROTOTYPE AND PRODUCTION PARTS
Machining covers 3-axis, 4-axis, and 5-axis CNC milling and multi-axis turning with live tooling, with materials spanning metals and engineering plastics — including aluminium alloys, stainless steel, copper alloys, brass, and plastics such as ABS, nylon, PEEK, and PPS. Secondary operations and surface finishing include anodizing, polishing, sandblasting, brushing, powder coating, electroplating, black oxide, and related processes. The scope is described in more detail on LKprototype's page for CNC machining for precision prototype and production parts.
DIMENSIONAL INSPECTION AND QUALITY DOCUMENTATION
LKprototype operates an ISO 9001-based quality management system and performs dimensional and visual inspection during and after production. Material certification is available from the raw material manufacturer, including heat number, grade, dimensions, mechanical properties, and chemical analysis, and a quality inspection report covering quantities, critical dimensions, threads and tolerances, and appearance can be provided with an order. For sensitive programs, confidentiality agreements are available and production areas operate under device restrictions.

SUPPORT FROM PROTOTYPE TO REPEAT PRODUCTION
The service model spans prototype machining, low-volume and small-batch production, and repeat orders, with the intent that the same engineering and inspection framework carries across the transition. That continuity is the practical benefit for a prototype-to-production program: the supplier that learned your tolerances, datum scheme, and critical characteristics during prototype work does not have to relearn them for the production order — provided, as this guide has argued throughout, that the production step is qualified on evidence rather than assumed from a successful prototype.
CNC MACHINING SUPPLIER SELECTION CHECKLIST
Use this as gate criteria, not as a wish list. An item without a satisfactory answer is a reason to pause at the stage indicated.
CAPABILITY, MATERIAL, AND TECHNICAL REQUIREMENTS
Machine type and axis count identified for this part, with the work envelope confirmed against the part and its fixture
The material and condition quoted match the specification exactly, including temper or grade
Comparable parts in this material documented, ideally with a dimensional report
Specific process route described, including setup count and how complex features are reached
Critical tolerances and geometric requirements identified by the supplier, not only by you
Measurement method proposed for each critical characteristic, with instrument identified
Finishing and secondary operations listed as in-house or subcontracted, with quality control described
Drawings and CAD reviewed before the price was issued, with DFM comments received
QUALITY, INSPECTION, AND DOCUMENTATION REQUIREMENTS
Quality certificate current, with scope naming the legal entity and site that will manufacture
Certification verifiable with the issuing body
Inspection equipment identified and calibration status confirmed
First article inspection scope agreed: which characteristics, which revision, which method
In-process inspection described for production quantities, with frequency and reaction rules
Material certificate type agreed, and traceable to lot or heat number
Documentation scope agreed for each shipment: certificate of conformance, dimensional report, material and process certificates
Nonconformance and corrective action process described
PRICE, LEAD TIME, AND COMMERCIAL REQUIREMENTS
Quote built on the correct drawing revision, material, finish, and quantity basis
One-time costs separated from recurring unit price
Inspection scope stated as included or excluded, never ambiguous
Lead time decomposable into stages, with the start trigger defined
Material availability assumption stated
Outsourced finishing inside the quoted lead time
Packaging specified and priced
Incoterm, freight, insurance, and duty responsibility stated
Quote validity, payment terms, and currency stated
Assumptions and exclusions written down
PILOT ORDER AND SUPPLIER QUALIFICATION REQUIREMENTS
Pilot order sized and scoped to the risk of the part and the newness of the relationship
Acceptance criteria defined in advance, with measurement methods agreed
Drawing revision for the pilot fixed and confirmed in writing
First article approved before production volume is released
Documentation tested during the pilot, not requested afterward
Deviation handling observed and assessed
Scorecard completed with evidence notes for each dimension
Weighting set before quotes were compared
Second-source or exit path identified, with the documentation needed to transfer
CNC MACHINING SUPPLIER FAQS
WHAT SHOULD I LOOK FOR IN A CNC MACHINING SUPPLIER?
Look for demonstrated fit between the supplier's machines, materials, and tolerances and your actual part, then for quality evidence that can be verified: certificate scope, calibration, inspection reports, and first article practice. Add engineering review before quoting, capacity for your volume, a lead time that can be decomposed into stages, and commercial transparency. Weight these by your project — a prototype and a production ramp do not need the same things.
HOW DO YOU EVALUATE A CNC MACHINING SUPPLIER?
Evaluate by turning every claim into a claim–verify–evidence test. A machining claim is verified by a machine list mapped to your part and a process route. A tolerance claim is verified by a dimensional report on comparable features. A certification claim is verified by scope, entity, and site. Then score capability, quality, engineering, capacity, delivery, communication, price, and risk on a consistent scale, and compare total delivered cost rather than unit price.
HOW DO I VERIFY A CNC MACHINING SUPPLIER?
Verify in three layers. Documents: certificate with scope, calibration records, material certificates, inspection reports on real parts. Interaction: technical questions at RFQ stage, revision control described, engineering contacts who can answer technical questions directly. Physical or live evidence: a video walkthrough or site visit showing the machines, the metrology area, and the material handling. Documents alone can be assembled; the three together are hard to fake.
HOW DO I KNOW IF A CNC SUPPLIER IS A REAL FACTORY?
Check identity consistency across quote, invoice, certificate, and shipping documents, then ask directly where the parts will be made and what is subcontracted. Ask what happens when a drawing question arises — a manufacturer answers technically; an intermediary usually routes the question externally. Request a live video walkthrough of the specific machine planned for your part. If an intermediary is involved, that is workable when disclosed and when quality responsibility is stated in writing.
WHAT CERTIFICATIONS SHOULD A CNC MACHINING SUPPLIER HAVE?
ISO 9001 is a quality management system standard. Certification can provide evidence that an organization operates a certified QMS within a defined scope, but it does not by itself prove that a specific part meets its drawing requirements.
HOW DO I COMPARE CNC MACHINING SUPPLIERS?
Lock the scope first: same drawing revision, material and condition, finish, quantity basis, inspection scope, and delivery terms. Then normalize each quote for unit price, one-time costs, inspection, finishing, packaging, freight and duty, commercial terms, and lead time. Record each supplier's stated assumptions and exclusions. Finally compute total delivered cost, including an allowance for rework and delay risk, and score the non-price dimensions separately.
HOW DO I QUALIFY A CNC MACHINING SUPPLIER?
Qualify in stages. Screen for capability fit against your part. Request evidence: certificate scope, calibration, inspection reports, material certificates, DFM commentary. Compare quotes on a normalized basis. Run a controlled pilot or first article with defined acceptance criteria and inspection methods. Approve the first article before releasing production volume. Then re-qualify when the process changes — new fixtures, new machine, material change, or drawing revision.
HOW DO I CHOOSE A CNC SUPPLIER FOR PRODUCTION?
Prioritize repeatability and process control over flexibility. Confirm fixture and programme control, in-process inspection with defined frequency, documented parameter and tooling management, material traceability, a change-control process, and nonconformance handling. Verify capacity, not just plant size: relevant machine time, scheduling, and inspection throughput. And confirm that the lead time accounts for outsourced finishing and shipping inside the quoted window.
SHOULD I CHOOSE A CNC SUPPLIER BASED ON PRICE?
Not on unit price alone, because the number that reaches your P&L is the total delivered cost of a conforming part arriving on schedule — including inspection, finishing, freight, duty, rework, and delay. A low quote that omits inspection scope or material certification is a quote for less work. Price is a legitimate factor among eight; it should be scored transparently alongside capability, quality, engineering, capacity, delivery, communication, and risk.
HOW DO I VERIFY CNC SUPPLIER QUALITY?
Verify quality through four layers of evidence: the quality system certificate with its scope and the entity manufacturing your parts; calibration records for the measuring equipment; a dimensional or CMM report on a comparable part showing actual values against drawing requirements; and a first article inspection on your own part with characteristic accountability and drawing revision identified. Ask for in-process inspection practice for production quantities, and for material certificates traceable to lot or heat number.
CONCLUSION: CHOOSE A CNC SUPPLIER BASED ON EVIDENCE, NOT PRICE ALONE
The suppliers that cause the most damage in a program are rarely the ones that cannot machine a part. They are the ones that answered every question convincingly and produced no evidence for any of it. Price alone does not distinguish between those suppliers and the ones that can actually deliver, because a low number and a missing inspection scope look identical on a spreadsheet.
Qualify on capability, evidence of quality, engineering support, capacity, delivery, communication, commercial transparency, and risk — and set the weighting before the quotes arrive, so the decision follows the priorities rather than the price. The best supplier is the one that can reliably meet your actual technical requirements and scale with the project, not the one that offers the lowest number.
The sequence that works is unglamorous and repeatable. Prepare an RFQ that states the scope explicitly, down to drawing revision, material condition, finish, inspection, and delivery terms. Request evidence from each supplier and check it: certificate scope, calibration, inspection method, material traceability, DFM commentary. Compare quotes on a normalized equal-scope basis and compute total delivered cost. Run a controlled pilot order or first article when the part's criticality or the relationship's newness justifies it, and approve it before releasing volume. Then scale on the evidence you have accumulated, rather than on the optimism generated by a single good prototype.
If you want a second opinion on a part before committing to a supplier, putting a drawing in front of an engineering team for DFM review and quoting — with your tolerance, finish, inspection, and quantity requirements stated — is the cheapest step in the sequence and the one that most often changes the decision.